Vibrocleaner
The evolution in fresh concrete recycling and aggregate recovery
PROBLEM
End-of-day residual concrete management, high disposal costs, and the environmental impact of concrete mixer truck wash water.
SOLUTION:
Vibrocleaner: A compact, automated unit that recovers 100% of the aggregates and clarifies wastewater for immediate reuse.
DISTINCTIVE FEATURES
- Total Recovery: Efficient separation of sand and gravel.
- Reliability: Guaranteed for 100,000 operating cycles without wear.
- Efficiency: Energy savings of over 50%.
- Clean Water: A closed-loop system that eliminates water waste.

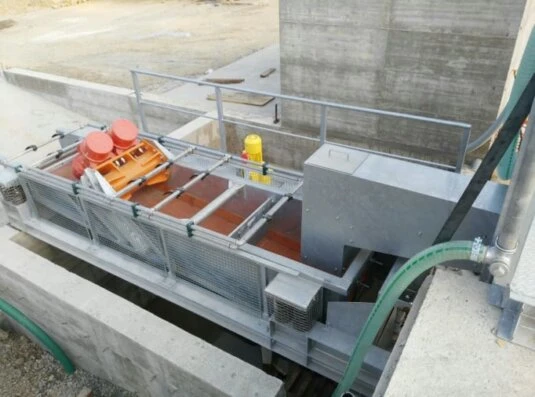
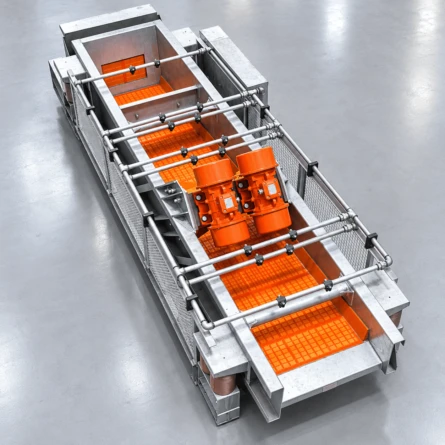
Vibrating frame
Robust hot-dip galvanized steel structure positioned above the storage tank.

Vibration Motors
Two powerful 5.0 kW motors ensure dynamic and efficient separation.

Spray nozzle system
A series of high-pressure spray nozzles for thorough washing of the aggregates.
OPERATION
How it works
The returned concrete is conveyed into the hopper.
The polyurethane mesh screen, driven by vibration motors, transports the material through the screening system.
At the same time, the spray nozzle system performs an intensive washing process that separates the cement paste from the solid aggregates.
RESULT
Recovered aggregates ready for reuse, while the slurry water is directed to the settling tank.
General Specifications
| Parameter | Value/Specifications |
Recovered aggregates ready for reuse, while the slurry water is directed to the settling tank. | 30 m3/h |
Vibration motor power | 5.0 kW |
Vibration motor power | 2300 Kg |
Operating voltage | Three-phase 400 V /50 Hz |
Storage tank | 4 x 6 m |
Screen mesh material | High-strength polyurethane |
Pump specifications
Submersible water dosing pump – Maximum flow rate | 40 m³/h |
Maximum operating pressure | 2 bar |
Submersible pump power | 5,5 kW |
Maximum operating pressure | 2 bar |
Submersible pump power | 2,2 kW |
Electric agitator specifications
Rotationvdiameter | 1,1 mm |
Power | 4kW |
Integrate Vibrocleaner into Your Plant!